Direct answer: A capable metal table leg manufacturer should convert the buyer’s application into a controlled drawing, material specification, approved sample, repeatable welding fixture, documented finish process, and lot-based inspection plan. Buyers should evaluate the complete manufacturing route—not only a catalogue photo or a sample that was hand-finished—because fit, stability, appearance, and repeatability depend on how each production lot is controlled.
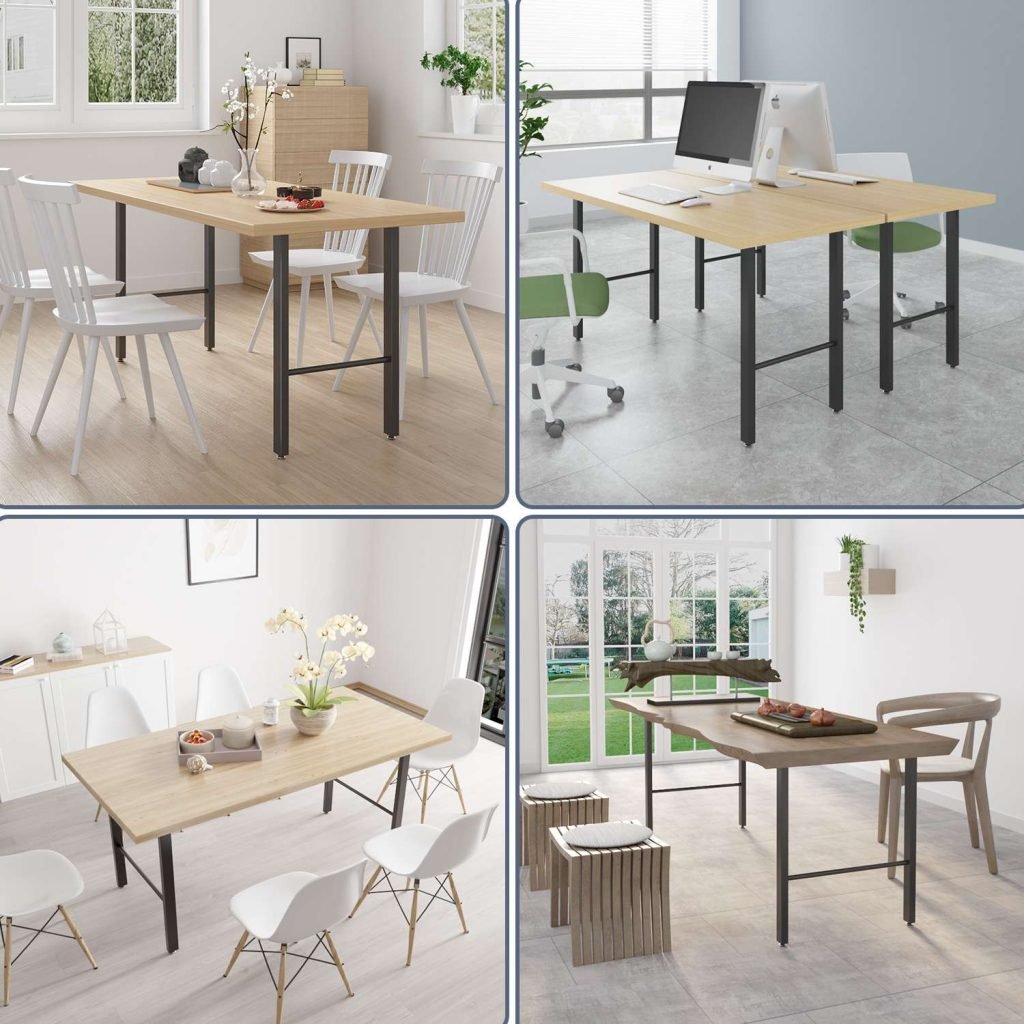
This guide helps furniture brands, importers, distributors, contract-furniture buyers, and OEM project teams define practical requirements for welded or fabricated metal table legs. It complements Jiansen’s industrial metal table-leg series, X-shape carbon-steel legs, and square steel-tube desk legs without assuming that any catalogue model fits every tabletop, market, or installation.
What should buyers specify to a metal table leg manufacturer?
Start with a revision-controlled technical package. A useful request for quotation identifies the table type, target market, tabletop interface, floor interface, material, geometry, finish, packaging, and required verification. A picture can communicate style, but it cannot define dimensions, tolerances, weld quality, or acceptance.
| Specification block | Buyer should define | Supplier should return |
|---|---|---|
| Application | Dining, office, café, bench, console, or project furniture; indoor or outdoor exposure | Application review and documented assumptions |
| Geometry | Overall height, footprint, tube or plate section, mounting-plate pattern, leveller interface | Controlled drawing and critical-characteristic list |
| Material | Material family, grade, condition, and permitted equivalents | Material evidence and lot traceability when required |
| Joining | Weld locations, joint type, permitted process, visible-surface expectations, repair rules | Process route, fixture plan, and inspection method |
| Finish | Surface preparation, coating or plating system, colour, texture, masking, appearance limits | Approved finish sample and process record |
| Validation | Assembly, stability, load case, fatigue or misuse scenario, acceptance criteria | Agreed test method and traceable report |
| Packaging | Unit protection, hardware segregation, labels, carton quantity, pallet and transport controls | Packing sample and packing-list reconciliation |
How should the controlled drawing be prepared?
The drawing should separate design intent from inspection requirements. Mark the dimensions that affect tabletop fit, floor contact, symmetry, interchangeability, assembly, and visible alignment. For each critical characteristic, define the nominal requirement, tolerance, measurement point, instrument or gauge, and inspection stage.
Control the tabletop interface
Specify mounting-plate size, hole or slot geometry, centre distances, edge distances, countersink details, fastener clearance, and any orientation marks. If several tabletop materials or inserts are used, identify each approved interface. A mounting pattern that works on one board construction may not be suitable for another.
Control height, footprint, and floor contact
Define overall height from the mounting surface to the floor contact, leg spread, foot position, leveller thread or insert, and allowable rocking or twist after assembly. For paired frames, specify how the pair is matched and how left/right orientation is identified.
Control visible geometry
Identify symmetry, angle, straightness, flatness, gap, and flushness requirements that affect furniture appearance. State which surfaces are customer-visible and which are concealed, because cosmetic acceptance should be tied to viewing conditions and surface class.
Which material controls should be included?
The bill of materials should identify the material grade or an approved equivalence procedure for tube, plate, inserts, levellers, fasteners, and accessories. Where chemistry or mechanical properties are important, define the certificate or independent verification required. Do not rely on colour, magnet response, or an undocumented supplier statement as material identification.
Traceability should be proportionate to risk and contract needs. The buyer can require a link between incoming material, work order, finished lot, inspection record, and shipment. If material is substituted, the supplier should submit the proposed grade, reason, technical comparison, affected quantity, and validation plan before use.
How should cutting, forming, and machining be controlled?
Tube cutting, laser cutting, punching, bending, drilling, tapping, and machining establish the geometry that the welding fixture must hold. Process plans should address tool wear, burrs, heat input, hole position, cut squareness, bend springback, and distortion. Characteristics that become inaccessible after welding or coating should be checked earlier in the route.
- Define datum surfaces and orientation before measuring hole patterns.
- Use go/no-go gauges where repeated interfaces justify them.
- Control burrs and sharp edges before welding or finishing.
- Protect threaded features from spatter and coating buildup.
- Record first-piece approval after tool, program, or fixture changes.
How should welding quality be managed?
Welding quality begins with joint design and process control, not final grinding. The drawing or welding instruction should identify joint locations, process, sequence, fixture points, visible requirements, prohibited discontinuities, and permitted repair. The supplier should control personnel competence, equipment condition, consumables, cleanliness, fit-up, heat input, distortion, and post-weld handling as relevant to the product.
ISO 3834-2:2021 defines comprehensive quality requirements for fusion welding of metallic materials in workshops and field installation sites. It is a useful reference for welding-quality systems, but citing the standard does not certify a particular table leg or replace the buyer’s product drawing, weld acceptance criteria, or validation plan.
Use fixtures to control repeatability
A fixture should locate the mounting plate, tube or frame members, feet, and accessories against defined datums. The control plan should state how the fixture is verified, how wear is detected, and what happens after maintenance or adjustment. Approved samples made without the intended mass-production fixture may not represent production capability.
Manage distortion before cosmetic finishing
Define checks for twist, rocking, mounting-face flatness, angle, and paired-leg symmetry before grinding and coating. Excessive correction can mask an unstable process. If straightening or weld repair is allowed, document the method, acceptance, and traceability.
Separate structural and cosmetic acceptance
Structural requirements address joint integrity and intended performance. Cosmetic requirements address weld profile, grinding transitions, spatter, pits, scratches, and visible consistency. Both should be agreed, but a smooth-looking weld is not evidence of internal integrity, and an acceptable structural weld may still fail a visible-surface standard.
How should the finish be specified?
Name the complete finish system rather than only a colour. The specification should cover surface preparation, pretreatment, coating or plating, colour reference, gloss or texture, masking, coverage, visible defects, cure or process verification, handling, and repair rules. State the intended environment and identify any project-specific test method and acceptance criterion.
If corrosion or adhesion testing is requested, define the specimen, preparation, exposure, evaluation, and pass/fail rule. A test method alone does not establish acceptance, and one result should not be converted into a universal outdoor service-life claim. The report must identify the actual part or coupon, finish system, lot, laboratory or test location, and agreed criteria.
What should be approved before mass production?
- Drawing release: close dimensions, materials, welds, finish, interfaces, labels, and packaging notes.
- First article: measure critical characteristics and record the actual results.
- Assembly trial: fit the legs to the buyer’s tabletop, inserts, fasteners, levellers, and mating hardware or controlled fixtures.
- Fixture approval: demonstrate that the intended production fixture controls geometry and orientation.
- Finish approval: retain a physical colour and texture boundary sample when appearance matters.
- Performance validation: run the agreed complete-system test with a controlled setup and documented failure criteria.
- Packaging trial: verify component separation, accessory count, labels, carton arrangement, and transport protection.
- Golden sample: identify revision, date, approval status, and storage responsibility.
Jiansen recommends that quotation, sample, purchase order, inspection report, and shipment records all reference the same drawing revision. A deviation should be approved in writing before production or shipment, even when the supplier considers it minor.
How should batch inspection be organized?
Divide inspection into identity, dimensions, workmanship, finish, assembly, function, packing, and documentation. Critical interfaces may need stricter control than minor appearance attributes. The purchase specification should define lot formation, sample selection, defect classes, acceptance and rejection rules, escalation, and disposition.
ISO 2859-1:2026 provides acceptance-sampling schemes indexed by an acceptance quality limit for lot-by-lot inspection by attributes. The standard helps select samples and make lot decisions; it does not define whether a weld, dimension, coating, or package is acceptable. Those product-specific criteria remain the buyer’s responsibility.
Define defect classes for the actual product
- Critical: an agreed condition that creates a safety, regulatory, or essential-function risk.
- Major: a condition likely to cause assembly failure, instability, loss of required function, poor interchangeability, or unacceptable visible quality.
- Minor: a departure from the workmanship standard that does not materially affect fit or function.
Include photographs or boundary samples for visual defects, but retain measurable drawing and process criteria as the controlling requirements.
How should performance be verified?
Validate the complete table system rather than assigning a universal capacity to a loose leg. Performance depends on the leg geometry, mounting plate, fasteners, tabletop construction, spacing, floor contact, levellers, load position, assembly quality, and use scenario. Define whether the test covers static, eccentric, cyclic, impact, stability, or foreseeable misuse conditions.
The protocol should identify the fixture, tabletop or representative interface, fasteners, load location, loading sequence, hold or cycle requirements, measurements, stop conditions, and failure criteria. A material certificate, weld record, or quality-system certificate does not by itself prove system performance.
Which supplier records should buyers request?
The required record set can include the approved drawing and bill of materials, deviation approvals, incoming-material evidence, first-article report, fixture check, in-process inspection, weld and finish records where required, final batch report, performance test report required by the order, packing record, and nonconformance disposition.
ISO 9001:2026 defines requirements for a quality management system. Certification can support process discipline, but buyers should verify the certificate scope, issuing body, validity, and supplying location. Certification does not replace product-specific evidence.
How should metal table legs be packaged?
Packaging should prevent metal-to-metal contact, finish abrasion, edge impact, moisture exposure where relevant, accessory loss, model mixing, and incorrect orientation. Define individual protection, corner or foot protection, hardware bags, quantity per carton, labels, barcode fields, carton and pallet arrangement, and any destination-specific packaging restrictions.
Before shipment, reconcile produced quantity, accepted quantity, packed quantity, carton quantity, accessories, and shipping documents. Approve a packing sample and controlled instruction before mass packing. Buyers reviewing broader China sourcing risks can also consult the existing table base manufacturer sourcing checklist.
How should engineering changes be controlled?
Require written approval before changing material source or grade, tube section, plate thickness, cutting program, fixture, weld process, subcontractor, pretreatment, finish, mounting pattern, packaging, or production location. The change request should state the reason, affected revision and quantity, technical comparison, validation evidence, inventory status, and implementation date.
For a controlled OEM review, buyers can submit drawings and application details through the Jiansen contact page. Open assumptions should be resolved before quotation so commercial and quality records describe the same product.
FAQ about metal table leg manufacturers
What should I send a metal table leg manufacturer for quotation?
Send a controlled drawing, application description, tabletop and floor interfaces, material and finish requirements, expected validation, inspection rules, packaging, and forecast or order context. Mark open items clearly so the supplier does not convert assumptions into undocumented production decisions.
How can a buyer assess welding repeatability?
Review the joint design, process instruction, production fixture, first-piece approval, fixture-verification method, in-process checks, distortion controls, repair rules, and batch records. A polished sample alone does not demonstrate repeatability.
Does ISO 3834-2 certify a table leg?
No. ISO 3834-2:2021 defines comprehensive welding quality requirements. It does not certify the performance of a specific table leg. Product conformity still depends on the approved drawing, process controls, inspection, and agreed system-level validation.
Which dimensions are usually critical?
Typical critical interfaces include overall height, mounting-plate flatness, hole and slot locations, leg footprint, angle, symmetry, floor-contact position, leveller interface, and paired-leg alignment. The buyer should define the exact tolerances and measurement methods for the project.
Can one load claim cover every tabletop?
No. A load claim should identify the tested leg, mounting plate, fasteners, tabletop construction, spacing, assembly, floor interface, loading method, and failure criteria. Changes to those conditions may require engineering review or new validation.
When should a new sample be approved?
Define triggers such as changes to material, geometry, tooling, fixture, weld process, subcontractor, finish, mounting pattern, packaging, or production location. The supplier should submit the change and validation evidence before implementation.
Conclusion
The best way to select a metal table leg manufacturer is to evaluate controlled production capability rather than a single attractive sample. Define the drawing, material, interfaces, welding and fixture controls, finish, sample approval, complete-system validation, batch inspection, packaging, traceability, and engineering changes before ordering. This creates objective quotation and acceptance criteria while keeping performance and certification claims within the available evidence.